
Read this article in 中文 Français Deutsch Italiano Português Español
Everllence secures first PARSYN compressor order
October 14, 2026
Electric motor-driven compressor train will support AM Green’s conversion of an existing ammonia production facility in Kakinada
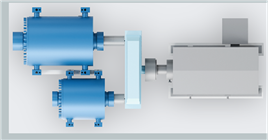 PARSYN compressor train for AM Green’s Kakinada project: two RB compressors (left), a gear box (center) and an electric motor (right). (Image:Everllence)
Everllence has secured its first commercial order for its PARSYN synthesis gas compressor train, which will be installed at AM Green’s green ammonia production project in Kakinada, Andhra Pradesh, India.
The order marks the first commercial application of PARSYN, a compressor train concept developed specifically for green ammonia production.
AM Green is converting an existing natural gas-based ammonia and urea production complex into a green ammonia facility. The Everllence compressor train will serve one of the plant’s production units, designed to produce 1,500 tons of green ammonia per day, or approximately 525,000 tons annually.
According to Everllence, that production capacity is expected to avoid approximately 1 million tons of CO₂ emissions annually compared with conventional ammonia production.
The first phase of the Kakinada project is planned to have an annual green ammonia production capacity of 1 million tons.
Compressor train designed for green ammonia
The PARSYN concept addresses differences between conventional ammonia production and facilities using renewable hydrogen.
Ammonia production requires hydrogen and nitrogen to be compressed before entering the high-pressure synthesis loop. Conventional ammonia plants typically use steam turbines to drive synthesis gas compressors, taking advantage of steam generated during the production of hydrogen from natural gas.
Green ammonia production generates substantially less process steam, making electric motor-driven compression an alternative.
PARSYN, short for parallel syngas compressor, incorporates two compressors arranged in parallel and connected through a gearbox. The arrangement allows each compressor to operate at a speed suited to its requirements while reducing the overall equipment footprint and improving maintenance access.
For the Kakinada project, Everllence will supply two barrel-type RB compressors, an electric motor, gearbox, dry gas sealing system, coolers, lubrication system, controls and instrumentation.
The scope also includes performance testing, dynamic simulation and process piping engineering.
“PARSYN is about more than choosing the right compressors. We looked at the entire train and how its components work together in a green ammonia plant,” said Markus Schürmann, senior sales and development manager, Green Ammonia, at Everllence.
Schürmann said the parallel arrangement enables a more compact compressor train and improved efficiency, potentially reducing both capital investment and operating energy requirements.
Manufacturing and delivery
Everllence developed the PARSYN concept and overall machinery train at its process gas compressor engineering operations in Oberhausen, Germany.
The RB compressors will be manufactured and performance tested in Zurich, Switzerland, while packaging and integration will take place in Oberhausen.
Delivery is scheduled for late 2027, with commissioning planned for 2028.
“The Kakinada project is a significant step towards producing green ammonia at industrial scale in India,” said Sunil Sharma, sales manager India at Everllence. “By converting existing facilities to use renewable hydrogen, AM Green is showing how established industrial infrastructure can become part of a lower-carbon production chain.”
International ammonia supply agreements
The Kakinada development is intended to supply international markets, including Germany.
AM Green has signed a long-term agreement with German energy company Uniper for the purchase of up to 500,000 tons of renewable ammonia annually from its projects. Initial shipments from Kakinada could begin as early as 2028.
AM Green also secured the Asian lot in an H2Global auction administered by Hintco, establishing a long-term purchase agreement for renewable fuels of non-biological origin (RFNBO) ammonia.
That agreement covers production from the second phase of the Kakinada project, with initial deliveries expected in 2029.
The compressor order represents an early commercial application of an electric motor-driven machinery train developed specifically to accommodate the process and equipment requirements of large-scale green ammonia production.
CONNECT WITH THE TEAM